EN


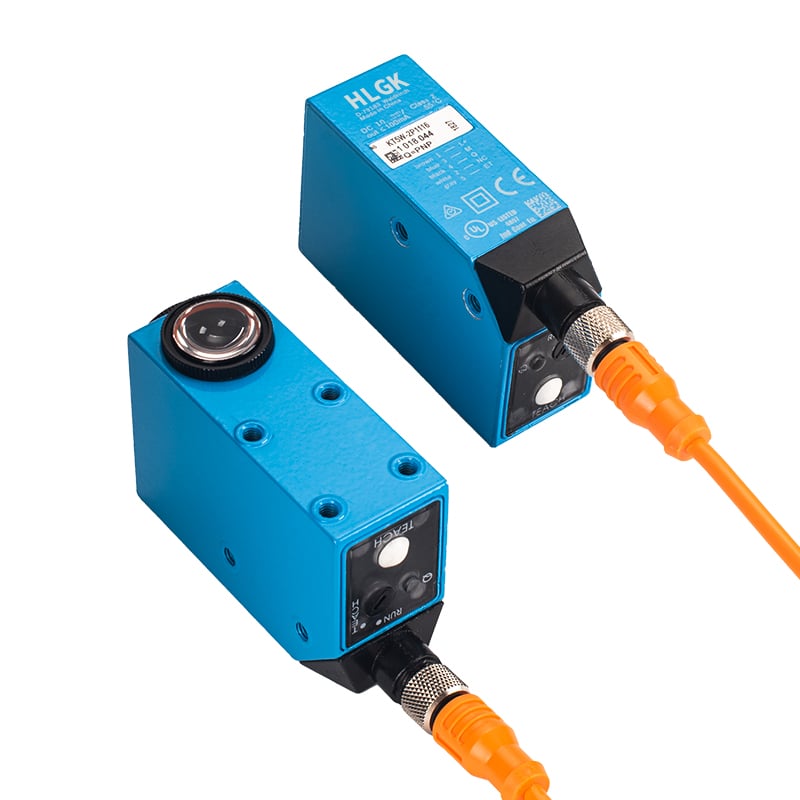
Understanding Color Code Sensor Technology
Core Principles of Color Detection
The way color detection works basically involves sensors reading different light wavelengths. Take the TCS230 sensor for instance, it measures how intense light waves are for various colors and turns this information into electrical signals. Getting good results really depends on having quality light sources because bad lighting just messes up what colors look like. Lighting from the surrounding area makes a big difference too, so most systems need either regular calibration checks or some sort of environmental controls put in place. From what we've seen in practice, getting color recognition right usually comes down to finding that sweet spot between all these elements, especially making sure there's consistent lighting throughout the setup.
Photoelectric Sensor Integration in Color Recognition
Photoelectric sensors play a big role when it comes to recognizing colors better, giving machines just the right level of control and sensitivity they need. Basically, these sensors pick up on how light changes when different colors move past them, which makes automated systems much more accurate overall. We see them all over manufacturing plants where they help separate items according to their color. Take the car industry for example, where companies rely on these sensors to make sure every part matches exactly what the design calls for in terms of color. Real world stats show that factories using these sensors end up with fewer mistakes and faster production times too. That's why so many manufacturers can't do without them anymore in today's automated world.
TCS230 vs. Advanced Sensor Models
Looking at how the TCS230 stacks up against newer color sensors reveals some pretty significant distinctions. The TCS230 has always been popular because it's straightforward to use and doesn't break the bank, which explains why educators and hobbyists gravitate toward it for classroom experiments and DIY projects. Inside, it relies on photodiode arrays to sense colors, but anyone who's worked with it knows there are limitations when dealing with different lighting conditions and getting proper calibration right. Modern alternatives tell a different story though. These advanced models come packed with better spectral response characteristics and much improved noise filtering, which makes them ideal for serious industrial work where accuracy matters most. Field tests consistently show these upgraded sensors deliver far greater reliability across various environments, something manufacturers have started noticing as they replace older equipment in production lines.
Key Features for Optimal Performance
Spectral Sensitivity and Resolution
The way color sensors respond to light at different wavelengths matters a lot for accurate color detection. When a sensor has good spectral sensitivity, it basically means it can tell apart colors more clearly because it reads the light intensity better across all those different wavelength bands. Then there's resolution too. This becomes really important when working in places where colors change fast. Sensors that have higher resolution just do a better job spotting small differences between colors, so they work more reliably over time. Take industrial settings for instance. High res sensors tend to pick up on color details much faster and across wider light spectrum ranges. This makes them much more dependable for things like product quality checks where even tiny color mismatches matter a great deal.
Environmental Tolerance (Dust/Moisture)
Environmental resistance matters a lot in manufacturing plants where sensors face tough working conditions daily. When dust builds up or moisture gets into equipment, sensors just stop working properly. That's why most industrial facilities look for sensors rated for harsh environments. Take IP67 ratings as an example these mean the device won't let dust inside and can handle being submerged in water for short periods. Without this kind of protection, sensors fail all the time, causing production delays and expensive repairs. We've seen plenty of cases where factories lost thousands because their sensors couldn't handle dusty air or occasional water exposure. Investing in durable sensors that actually work under real world conditions helps manufacturers avoid downtime and keeps their operations running smoothly even when things get messy on the factory floor.
AC Relay Compatibility for Industrial Use
Getting AC relay compatibility right matters a lot when bringing color code sensors into older industrial setups. When sensors don't match up properly, it creates headaches for automation workflows because extra workarounds become necessary or integration just doesn't happen smoothly. On the flip side, sensors that actually work with AC relays make things run much better overall. Take manufacturing plants for example many factories have reported major improvements after switching to sensors that talk to standard relays without issues. The real value comes from how these compatible sensors fit right into existing automation frameworks, which means color detection works as part of the bigger picture instead of standing alone. Plants that got this sorted out saw their production lines move faster while maintaining quality standards across different product runs.
Integration with Industrial Control Systems
Micro Limit Switch Synchronization
Micro limit switches play a key role in many automation setups, particularly when working alongside color code sensors. Basically, these little devices help figure out if something is there, gone, or where it should be, which makes the whole system react faster to changes. When we get these micro limit switches to work hand in hand with color code sensors, the whole automation process gets a lot better because specific actions kick in right when needed after detecting an object. Take one factory I know about - they started syncing their switches with color sensors and saw real gains in how much stuff got done. Products could now be tracked and sorted automatically based on colors, cutting down errors and saving time across the production line.
Electrical Relay Interfacing Best Practices
Interfacing electrical relays with color detection sensors requires careful adherence to best practices to ensure optimal performance and reliability. Some key practices include:
- Correct Relay Selection: Choose relays with adequate voltage and current ratings to match the sensor's requirements.
- Secure Connections: Ensure all connections are secure to prevent signal loss or electrical issues.
- Diode Protection: Use diodes for relay coils to protect the circuit from voltage spikes.
- Isolation: Implement isolation between the relay and sensor circuits to prevent interference.
These practices help avoid common mistakes like incorrect relay type choice or poor connection setup, which may lead to functional failures. By consulting expert opinions and industry guidelines, such as those from electrical engineering standards committees, one can effectively optimize relay interfacings, thereby enhancing system integration reliability.
PLC Communication Protocols
PLC communication protocols play a vital role when it comes to integrating color code sensors into industrial systems. These protocols enable smooth data transfer and control signals between the PLC unit and various sensors, which is essential for making timely decisions on factory floors. Industry favorites such as Modbus and CAN have become go-to options because they work reliably across different equipment setups. Take Modbus for instance – it provides straightforward communication paths between sensors and PLCs so data gets transmitted accurately without delays. We see this in action all the time in automotive plants where these protocols keep production lines running smoothly. When manufacturers implement these communication standards properly, they get better sensor integration results that boost overall automation efficiency and help manage complex processes day after day.
Calibration Techniques for Accuracy
White Balance Adjustment Strategies
Getting the white balance right makes all the difference when it comes to accurate color detection because it helps sensors see colors properly no matter what kind of light they're working under. When adjusting white balance, we're basically telling the sensor what white actually looks like so everything else falls into place naturally. People use different approaches for this too some grab white reference cards while others rely on automated tools built into their equipment these days. Industry guides generally suggest keeping lighting consistent across scenes and doing regular checkups on those sensors to keep things running smoothly. A well calibrated system means better results whether someone is taking photos or managing complex automation processes in manufacturing settings.
Frequency-to-Color Mapping Methods
Mapping frequencies to colors is really important for getting accurate readings from sensors since it converts those raw frequency outputs into colors we can actually see and understand. The way this works generally depends on some pretty clever tech stuff like special algorithms or pre-set tables that match certain frequencies to specific digital color codes. How exactly this mapping happens makes a big difference too many times what comes out at the end just isn't reliable enough for proper color recognition. Looking at what various labs have found lately shows us that better mapping approaches tend to boost how well these sensors work overall. They get more accurate results whether there's lots of light around or not much at all which matters a lot in real world applications where lighting conditions aren't always perfect.
Environmental Compensation Algorithms
Things like ambient light levels and temperature changes tend to mess with color detection readings, so most systems need some sort of compensation algorithm built in. These smart adjustments basically tweak what the sensors pick up based on what's going on around them, which helps keep colors looking right no matter what. Most manufacturers go with either adaptive threshold calibration or adjust for changing light conditions as they happen. We've seen this work pretty well in lab tests where they simulate different lighting situations. When sensors can factor out these environmental quirks, they give much better results whether installed inside a factory or used in home devices. For instance, medical equipment relies heavily on accurate color readings despite varying room conditions throughout the day.
Practical Applications in Automation
Color-Based Sorting Systems
Color sensors are changing how sorting works in many different sectors from manufacturing to food processing. When companies install these devices, they basically get machines that sort items by color automatically instead of relying on people to do it manually. Take the TCS3200 model for instance it can pick out all sorts of colors really well, which makes it great for factories where quick accurate sorting matters most. Real world tests show pretty clearly that when businesses switch to color based sorting systems, they need far fewer workers doing the tedious task of picking through products by hand. Plus things move through the system much faster, cutting down on expenses while getting more done in the same amount of time.
Quality Control Inspection Setups
Color detection plays a big role in quality control when it comes to keeping product standards high through consistent coloring and accurate matches. Take the TCS3200 sensor for instance it stops those weird colored items or ones that don't meet specs from getting shipped out, which protects the brand's reputation and keeps customers happy. According to industry data, companies that install these kinds of sensors typically see better results across their quality checks. Less waste ends up happening too since problems get caught earlier in the process. Studies actually show defect rates drop quite a bit after installation, proving these sensors can spot even small color differences fast enough to make a real difference on the factory floor.
Travel Limit Switch Coordination
When travel limit switches work together with color code sensors, automated systems can really step up their game. These switches basically keep things running smoothly by making sure components stay within set limits. Pair them with color sensors though, and suddenly there's all sorts of extra capabilities. The system can actually trigger actions based on what colors it detects. Take conveyor belts for example. Some factories have combined TCS3200 sensors with travel limit switches on their lines, and guess what? Productivity goes way up because these setups spot objects correctly and activate the right switches at just the right time. Companies that tried this out noticed their equipment lasted longer too, plus their automation became much more accurate overall. It turns out combining these different sensing technologies creates some pretty good results across manufacturing operations.