EN


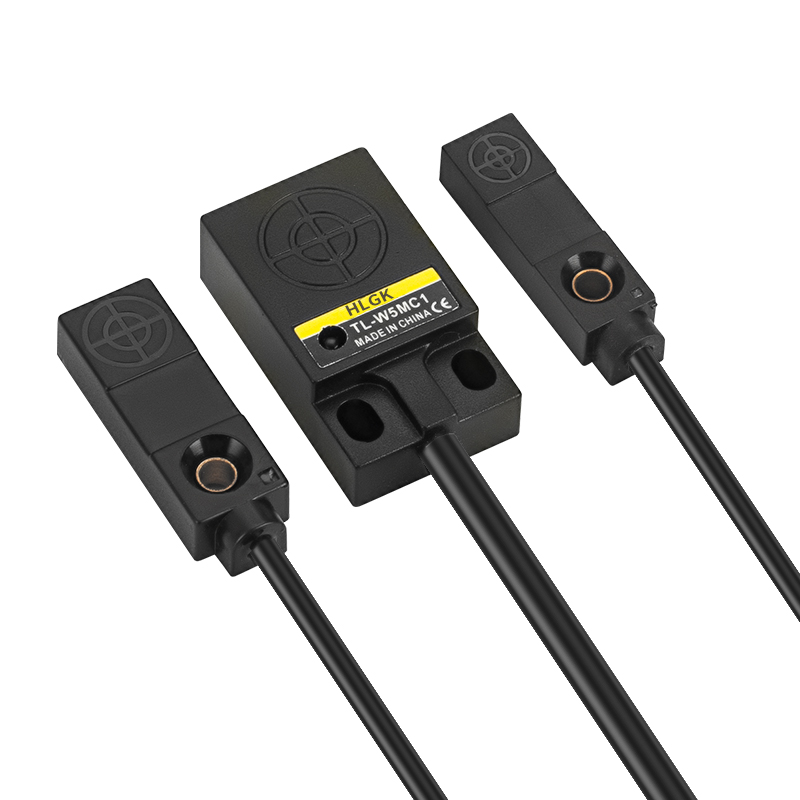
How Photoelectric Sensors Enhance Automation Efficiency
Core Mechanisms of Photoelectric Sensing
Photoelectric sensors play a big role in automated systems, basically working by shining light to tell if something is there or not. At their core, these sensors send out a light beam and watch for either reflections coming back or when the beam gets blocked completely. As objects move across this path, the sensor notices those changes in light patterns, which tells it where things are located. Getting the right light modulation matters a lot too since it helps sensors spot objects clearly even when conditions aren't perfect. Most modern sensors work with different types of light waves, going from invisible infrared all the way up to what our eyes can see. This range makes them pretty adaptable for all sorts of situations, performing well both in dark corners of factories and bright outdoor settings where sunlight might otherwise interfere.
Research shows that adding photoelectric sensors makes operations run better than before. Take factory assembly lines for example, where these sensors cut down mistakes during product handling, which keeps everything moving without constant stoppages. They basically take over tasks people used to do manually, so workers aren't constantly checking things and the whole process becomes much more accurate. The boost in efficiency means factories produce more goods while spending less time fixing errors. Many manufacturing plants now rely heavily on these sensors because they help keep up with customer expectations for faster delivery times. In today's world of smart factories, photoelectric sensors just make sense for anyone wanting reliable performance day after day.
Through-Beam, Retroreflective, and Diffuse Sensor Types
Photoelectric sensors come in three primary varieties: through-beam, retroreflective, and diffuse, each with unique advantages that boost automation performance. The through-beam type works by positioning an emitter on one side and a receiver on the opposite side, so objects trigger detection simply by breaking the light path between them. Industry professionals often favor these because they deliver exceptional accuracy and can work across considerable distances, which makes them perfect for situations needing pinpoint detection over extended ranges. Then there's the retroreflective option, which combines both emitter and receiver into one compact housing. When light hits a reflective surface, it bounces back to the sensor, creating a detection signal. Many technicians appreciate this design since it cuts down on installation time and maintenance headaches, all while reliably handling medium distance sensing requirements in manufacturing environments.
Diffuse sensors operate by bouncing out light that hits objects and then comes right back to them, making them great for detecting things up close. They really shine in situations where what needs to be detected changes colors or has different reflective surfaces. The way they react to various materials makes automated processes much more adaptable in real world conditions. Industry data shows businesses that switch to these kinds of sensors tend to see better results when it comes to reliable detection. One recent study found that factories employing both retroreflective and diffuse sensors saw fewer mistakes during production runs, which speaks volumes about how these technologies help streamline operations across manufacturing floors.
In conclusion, the diverse applications of these sensor types cater to various industry needs, ensuring efficient automation tailored to specific operational demands.## Critical Applications in Modern Industrial Systems
Object Detection in Conveyor and Packaging Lines
Photoelectric sensors have become a vital component in today's industrial operations, especially for spotting items moving along conveyor belts and packaging lines. When factories install these sensors, they get better control over product movement which keeps production running smoothly most of the time. These sensors basically tell the system when something arrives at a particular point on the line, so there are fewer mistakes and less backup happening. Real world data shows plants that upgraded their systems saw downtime drop by around 30% last year according to recent manufacturing surveys. With pressure mounting on manufacturers to crank out more goods faster, adding photoelectric sensors makes sense for improving how things run day to day while still keeping those quality checks intact during the packaging process.
Precision Positioning in Robotic Assembly
Photoelectric sensors play a key role in getting those tight tolerances right during robotic assembly work. These sensors detect objects and align components so precisely that robots can put together products with very few mistakes. Take automotive manufacturing for instance - when photoelectric sensors guide part placement on production lines, they help maintain uniform quality across thousands of units. Industry professionals have seen time and again how adding these sensors boosts overall accuracy rates. Factories waste less material and make better use of their resources when everything fits just right from the start. The bottom line? Companies save money while still hitting those tough quality standards customers demand nowadays.
Safety Interlocks and Machine Guarding
Adding photoelectric sensors to safety interlocks and machine guarding systems plays a critical role in keeping workplaces safe. These devices offer dependable detection of potential dangers and activate safety responses that protect workers and equipment alike. Major safety standards bodies like OSHA recommend photoelectric sensors as essential components for meeting safety regulations and reducing accident rates on factory floors. When someone breaks the light beam from these sensors, it signals an unexpected presence near dangerous machinery parts, which triggers automatic shutdowns before any harm can occur. Companies that install these kinds of safety features not only improve worker protection but also shield their expensive equipment from damage, all while staying within legal requirements for occupational safety.
Non-Contact Operation and Reduced Maintenance
In industrial settings, photoelectric sensors stand out because they work without touching anything, which means less maintenance overall. These devices detect objects through light rather than physical contact, so there's no wear and tear on parts like mechanical switches tend to have. The result? Much longer periods between needed repairs and lower repair bills. Some factory managers report savings around 30% on maintenance when switching to these non-contact options. Beyond just saving money, this setup keeps production lines running smoother too since machines don't break down as often during operations.
High-Speed Performance in Dynamic Environments
What really stands out about photoelectric sensors is how fast they work in all sorts of changing environments. These little devices can pick up on changes almost instantly, which makes them perfect for those super fast production lines we see these days. Take a look at the numbers behind them too mind blowing stuff actually. Some models respond within just 30 microseconds! That kind of speed lets them keep up with situations that change from second to second without missing a beat. We've seen this firsthand in places like package sorting centers where every millisecond counts, or along conveyor belts moving products at breakneck speeds. The combination of quick reaction time and reliable operation has made these sensors indispensable in modern manufacturing setups.
Environmental Interference Solutions
Getting photoelectric sensors to work properly faces some pretty big hurdles because of all sorts of environmental stuff getting in the way. Dust builds up on those delicate lenses, fog messes around with the light beams, and shiny surfaces just bounce everything back where it shouldn't go. When dust gets stuck on the lens, it blocks the path of the light completely. Fog does something different but equally bad by scattering the beams all over the place which leads to wrong readings. Shiny floors or walls create problems too since they reflect the beam instead of letting it pass through normally. The good news is manufacturers have come up with ways to fight back against these issues. Many modern sensors now come equipped with automatic cleaning systems that wipe away dirt buildup between operations. Some models even shoot out beams strong enough to cut through thick fog and dusty environments. There's also this cool tech called polarized filters that actually helps tell real signals apart from unwanted reflections, making sure what gets detected is really there.
Integration with Micro Limit Switches and Timer Relays
When photoelectric sensors get combined with micro limit switches and timer relays, automation control systems tend to work much better overall. The way this works is pretty straightforward really. Sensors connect to those tiny limit switches that spot exact points where machines should stop moving. This matters a lot for keeping things within safe operating ranges. Add timer relays into the mix too, since they handle timed tasks. Together, all these parts create a system that only starts working when everything else is ready to go, cutting down on wasted movements and saving resources along the way. Take assembly lines for instance. When properly integrated, these systems wait until one part finishes before moving another piece along the line, making production run smoother day after day. Factories across different sectors have seen real improvements in how efficiently they operate while also becoming safer workplaces. Combining these technologies creates some pretty good results in practice. Companies report faster response times from their equipment and fewer breakdowns requiring maintenance, which ultimately means more products getting made without delays.
Smart Sensors for Industry 4.0 Integration
Photoelectric sensors are playing a bigger role in Industry 4.0 these days, mainly because they let manufacturers connect things to the internet of things (IoT) in ways that weren't possible before. What makes them special is their ability to monitor conditions instantly and send back data that actually matters for running factories better. When plants install these smart sensors, they get all sorts of systems talking to each other without hiccups, which means managers make smarter choices faster and equipment breaks down less often. Looking at what's happening in the market right now, more factories are jumping on board with these sensors since they see how much difference they can make in day to day operations. Research shows we should expect even more installations over time, mostly because businesses want to save money on resources while keeping workers safer during production runs.
Emerging Applications in Autonomous Systems
Photoelectric sensors are changing how autonomous systems work, especially in cars and flying drones. These sensors can spot things in their path pretty accurately and help figure out where they're going, which makes all sorts of tech safer to operate. When installed on vehicles, they keep track of where the machine should go and what's around it, cutting down on mistakes people might make while driving or piloting. Some studies show that sensor tech will keep getting better over time, and many engineers think we'll see even more photoelectric sensors built into new gadgets and machines soon. As these sensors become more common across different kinds of automation, they're raising the bar for both safety measures and operational efficiency while pushing forward some pretty cool technological advancements that could change our relationship with automated devices altogether.
---
Through these innovations, photoelectric sensing technology is paving the way for smarter, safer, and more efficient industrial processes and autonomous solutions. Whether in the context of Industry 4.0 or cutting-edge autonomous applications, photoelectric sensors continue to prove their indispensable value in modern technology landscapes.
Table of Contents
-
How Photoelectric Sensors Enhance Automation Efficiency
- Core Mechanisms of Photoelectric Sensing
- Through-Beam, Retroreflective, and Diffuse Sensor Types
- Object Detection in Conveyor and Packaging Lines
- Precision Positioning in Robotic Assembly
- Safety Interlocks and Machine Guarding
- Non-Contact Operation and Reduced Maintenance
- High-Speed Performance in Dynamic Environments
- Environmental Interference Solutions
- Integration with Micro Limit Switches and Timer Relays
- Smart Sensors for Industry 4.0 Integration
- Emerging Applications in Autonomous Systems